Active coils
The coils of a spring that actually flex under load, as opposed to the total count including closed-end coils. Rate is set by the active coils, which is why end style and coil count travel together on a specification, and why two springs of equal total coils can behave differently.
Buckling
The sideways bowing of a compression spring that is too slender for its deflection, a geometry problem, not a defect. Slender springs need guiding, a rod inside or a hole outside, and the need is predictable at design time, so tell your spring maker how the spring is supported.
Closed and ground ends
Compression spring end treatments: closed ends seat the spring; grinding them flat makes it stand square and load evenly. Grinding adds cost and is not automatic, so specify it where squareness and even loading matter, at larger wire sizes especially, and skip it where a seated coil is enough.
Coiling
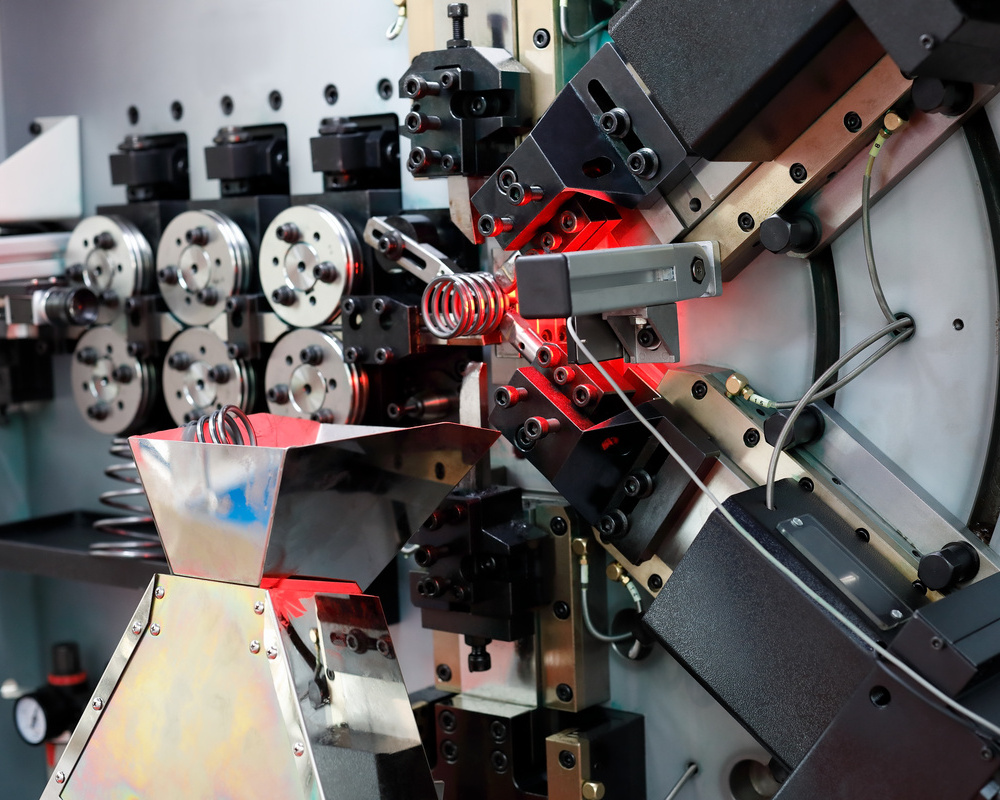
The forming of springs on CNC coilers, programmed rather than tooled, which is the sector's defining economics: no dedicated die, modest setup, and the same machine making one spring or a hundred thousand. It is why custom springs are reachable at low volumes in a way custom stampings are not.
Commercial tolerances
The published baseline tolerances of the trade, SMI's tables grading loads, rates, and dimensions by normal manufacturing variation, that a quote assumes when a print does not say otherwise. Writing commercial tolerances per SMI's published guidance on the drawing is a real, citable instruction, and tightening past it is a priced decision, not a title block habit.
Compression spring
The helical spring that resists being squeezed, the sector's staple, specified by wire, diameters, free length, rate or loads at heights, ends, and material. Most of this page's vocabulary exists to describe it precisely, because a compression spring is easy to buy and easy to buy wrong.
Conical spring washer
The dished washer, commonly called a Belleville washer, acts as a very stiff, short-travel spring, used singly or in stacks that add travel or load depending on orientation. It solves high-load, small-space problems that bolted joints and preloads create, and stacking arrangement is part of its specification, not an assembly afterthought.
Constant force spring
A coil of prestressed flat strip that pays out with nearly uniform pull over long travel, the counterbalance and retractor workhorse. It is specified by force, travel, and life; its strip-based cousins live here rather than with stamping, because the spring is the product and the mounting drum diameter is part of the design.
Die spring
The heavy-duty rectangular-wire compression spring built for die and mold service, supplied in standardized sizes and color-coded duty classes as a catalog product. Die springs are bought by envelope and duty from stock, a reminder that this sector has a large catalog side alongside its custom work.
Direction of wind
Whether a spring's helix is right-hand or left-hand is irrelevant until it is critical: torsion springs load in the direction that winds them tighter, nested compression springs alternate hands so that coils cannot tangle, and springs threading onto parts must match them. Say the hand when any of these apply.
Extension spring
The helical spring that resists being stretched, with hooks or loops at its ends and, usually, initial tension holding its coils closed. The hooks are the hardest part of the design and the usual failure point, which is why hook geometry deserves as much attention as the body.
Free length
A spring's unloaded length, the reference from which deflections are measured. It is also one of the most overconstrained dimensions in the sector: if loads at working heights are specified, free length can often float commercially, and letting it float is one of the easy ways to buy springs better.
Hooks and loops
The end formations of extension springs- full loops, side loops, extended hooks, machine hooks- each with its own stress concentration and cost. Hook stresses commonly exceed body stresses, so hook style is a durability decision, and a cyclic application may do better with threaded plugs or reduced-stress ends than with the default loop.
Hot-wound springs
The heavy end of the trade: above roughly half-inch wire, springs are wound hot from heated bar by a separate, smaller set of manufacturers, with their own heat treatment, their own tolerances under the hot-coiled spring standard, and longer lead times. Suspension, rail, mining, and press springs live here, and the sector's no-tooling economics do not, so heavy work is sourced by naming the segment, not by shrinking a coiler search.
Index
The ratio of the mean coil diameter to the wire diameter is the spring maker's difficulty number. Moderate indexes coil sweetly; very low indexes strain the wire and the coiler, and very high ones make floppy, hard-to-control springs. When a design review nudges a diameter, the index is usually what it is rescuing.
Initial tension
The preload is wound into a close-coiled extension spring that holds its coils shut until the applied load exceeds the spring's load limit. It is a real, specifiable, toleranced quantity, the reason an extension spring's load line does not start at zero; and it varies with manufacturing more than the rate does, so tolerate it realistically.
Load at height
The specification style that states what the spring must do: a load at a working height, or better, loads at two working heights, which together fix the rate through the working range. It is the honest way to buy function, and it beats overconstraining geometry, because the maker can then engineer wire, coils, and free length to deliver it.
Music wire
The high-carbon, cold-drawn steel spring wire of the workaday spring world, made to a music-spring-quality specification for high stresses and good fatigue properties. It is the default answer at small wire sizes, uncoated and rust-prone, so service conditions, not habit, should confirm it.
Passivation
The chemical treatment of finished stainless springs that removes free iron picked up during forming and restores the passive surface, performed in accordance with standard passivation practices. Stainless that rusts in service usually skips it, so passivation belongs on the purchase order for corrosion-critical stainless work, not assumed.
Presetting
Compressing a spring beyond its elastic limit once, deliberately, so it takes its set at the factory rather than in service, stabilizing the free length and raising the load-carrying capacity. Also called set removal, it costs an operation and is specified, not assumed, for springs that work near their limits.
Rate
The spring's stiffness: load per unit deflection for compression and extension; torque per unit angle for torsion. Rate is a derived property of wire, diameter, and active coils, toleranced more loosely than dimensions, and specifying rate plus one load, or loads at two heights, is usually the cleanest complete statement of function.
Shot peening
Bombarding a spring's surface with media to leave compressive residual stresses that slow fatigue crack initiation, the standard life-extending treatment for cyclic springs. It is specified with process control for fatigue-critical work, and it is one reason two visually identical springs can have lives that differ by orders of magnitude.
Solid height
The length of a compression spring with all coils touching, the geometric floor of its travel. Designs need clearance above it, or deliberate use of it as a stop, and solid height plus required travel plus loaded height must all fit the envelope, which is where many spring specifications quietly contradict themselves.
Stress relieving
The low-temperature heat treatment after coiling, which relieves the wire's residual stresses and stabilizes dimensions, is standard practice in competent spring making, not an extra step. It is worth knowing about, mostly so its absence in the cheapest possible quote can be recognized for what it is.
Torsion spring
The helical spring that resists rotation, delivering torque through legs whose geometry, length, angle, and mounting are half the design. Torsion springs are specified by torque at angular positions; they prefer loading in the winding direction, and they work best over a supporting shaft sized with the spring's tightening in mind.
Valve-spring-quality wire
The cleanliness tier of the wire specifications: the same chemistries held to cleaner steelmaking, tighter surface standards, and closer inspection, bought when fatigue life is the mission, because fatigue cracks start at inclusions and surface flaws. It exists as a separate sibling specification alongside the standard grades, and naming the tier is how a print buys cycle life rather than hoping for it.
Wave spring
A flat-wire spring of waved coils delivering compression-spring loads at a fraction of the axial space, the answer when work height is the scarce resource. Wave springs trade travel and simplicity for compactness, and they are specified by load at work height and the cavity they must live in.
Wire form
The catch-all for bent-wire products that are not helical springs: clips, rings, hooks, guards, racks, and custom shapes, made on CNC wire benders and fourslide machines. Wire forms are specified by print, wire, and finish, and this sector owns them; strip-based fourslide parts belong to the stamping sector.