Back to All Buyer's Guides Sectors

Industrial Web Search Buyer's Guide Sector

Electronics Manufacturing Services & PCB Assembly

Contract manufacturing of electronic hardware: bare printed-board fabrication, board assembly by surface-mount and through-hole processes, and full-service EMS through box build, test, and fulfillment. This sector covers the fabricators, assemblers, and EMS providers that supply it; the IPC class and acceptance system that specifies the work; and the turnkey-versus-consigned commercial structure that determines who carries the component market's risk.

Overview

How the Electronics Manufacturing World Divides, and Who Builds What

Orientation before the RFQ: three different purchases share this sector's name, and sending the right package through the right door is most of the first battle.

Send bare-board files to an assembly house, and you will be politely redirected; send an assembly RFQ to a board fabricator, and the same thing happens in reverse. The industry enforces its own first sorting, and it has three doors. Bare-board fabrication builds the unpopulated printed board from your fabrication data, a chemical, drilling, and plating business with quick-turn domestic shops at one end and volume fabrication, much of it offshore, at the other. Assembly populates boards: solder paste, placement, reflow, and the through-hole and selective processes behind them.

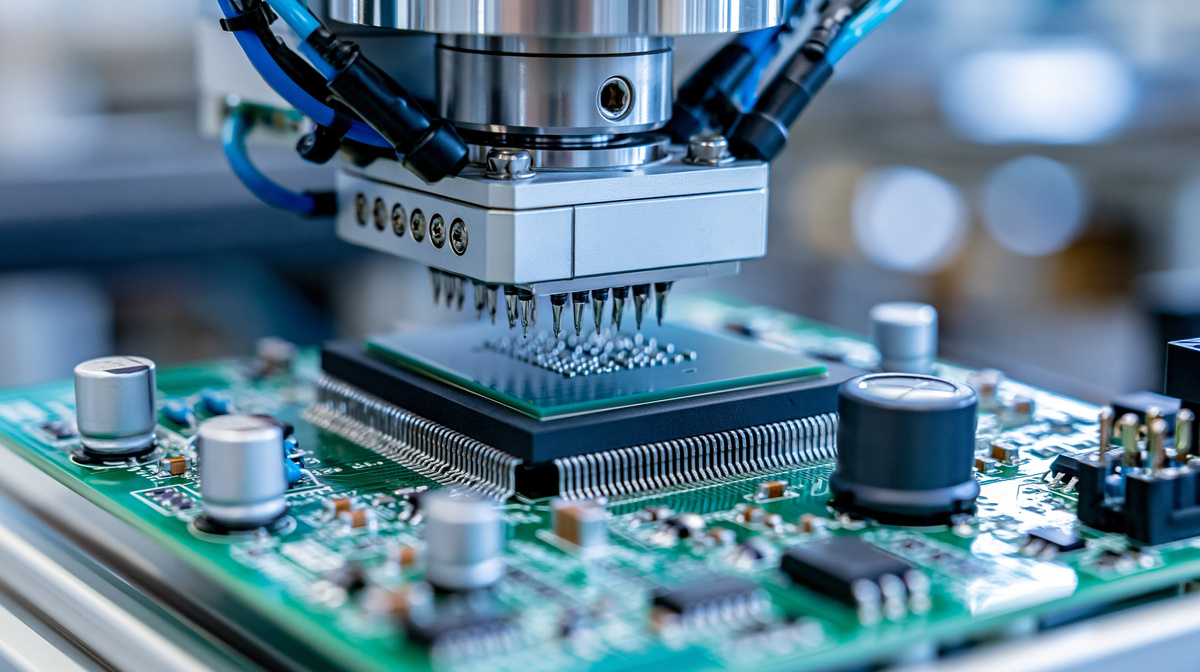
Automated SMT line placing electronic components onto printed circuit boards during production.

And full-service EMS wraps assembly in everything around it: component procurement, box build, test engineering, and fulfillment, up to finished products shipped under your label. Then comes the sentence this page most wants remembered: two axes decide who inside each door can bid at all. The first is the technology floor: the finest pitch, the center-to-center spacing of a package's leads, the smallest passives, hidden-joint packages, and any HDI construction on the design, each shrinking the qualified field. The second is the volume-and-mix band: prototype and NPI shops, high-mix mid-volume houses, and high-volume lines are different businesses, staffed and tooled differently, wearing one industry's name. Place your design on both axes before building a bid list, and the rest of this page gets easier.

This sector runs on a package of files and a shared grading language. The design data, fabrication files, the bill of materials with its approved manufacturers, drawings, and placement data are the specification; quotes are priced from it, and its completeness is the difference between a two-day quote and a two-week correspondence. The grading language is IPC's class system: Class 1 for general electronics, Class 2 for dedicated-service equipment that must be reliable, Class 3 where failure injures or ends missions, written into orders by standard, revision, and class, with the full high-reliability string naming the board, the soldering process, and the acceptance criteria together. And beneath the paperwork runs the commercial spine: turnkey, where the assembler buys the components, or consigned, where you do, a decision about who carries the component market, its lifecycle endings, its recurring allocation cycles, allocation being the industry's word for demand outrunning supply until makers ration deliveries, and its gray-market hazards, more than about the board itself.

Four kinds of companies supply the sector. Bare-board fabricators build the boards, sorted by technology, HDI capability above all, layer count, and turn time. Contract assemblers and EMS providers run the lines, from NPI specialists through high-mix houses to volume operations, with the larger ones offering design-for-manufacturability review, test development, and box build as standing services. Component distribution feeds everyone: franchised distributors carrying manufacturer-authorized stock with its warranty and traceability, and the independent channel, brokers, and the gray market, useful in shortages and the doorway counterfeits use, which is why channel policy is a specification item. Test and inspection houses, plus design services around NPI, fill the gaps for buyers who need engineering without a factory attached. The routing follows the scope: board files to fabricators, boards plus BOM to assemblers, products to EMS partners, and parts questions to the distribution tier whose traceability matches your risk. The boundaries are clear, each with its own page here: cable and harness assemblies are a sibling sector with their own acceptance standard, enclosures and chassis come from sheet metal fabrication, and medical device work adds a regulatory regime covered on the medical device contract manufacturing page. Your choice determines who owns the yield, the schedule, and the two-in-the-morning phone call when a lot misbehaves.

Sourcing Considerations

How to Buy Electronics Manufacturing: 6 Things to Get Right

Six decisions, in the order the quotes will force them anyway. The first two decide which companies belong in the conversation; the other four decide how well the winner performs.

01

Sort the purchase before the RFQ: board, assembly, or product

Decide what you are actually buying, bare boards, assembled boards, or a finished, tested product, and send the package through that door, because each scope has its own supplier base, quoting language, and pricing logic. Then place your design on the two sorting axes, technology floor and volume band, before building the bid list. RFQs sent to the wrong tier do not get declined; they get quoted badly, and the badness surfaces at first article.

02

Write the class, not the wish

Put the acceptance class in writing: the standard, the revision, and Class 1, 2, or 3 on the drawing or purchase order, with per-reference-designator exceptions where one circuit is critical and the rest is not. For high-reliability work, name the full string, board, soldering process, and acceptance, each at the class. Workmanship described in adjectives is negotiated at inspection; workmanship named by class was purchased.

03

Treat the BOM as the contract

Quote from a complete bill of materials: manufacturer part numbers, approved manufacturers and pre-approved alternates per line, reference designators, and do-not-place notes, screened for lifecycle before release. Quote every ambiguous line with an assumption, treat every end-of-life part as a redesign rehearsal, and approve every alternate in advance so a shortage won't stop the line. The BOM is where programs are actually won.

04

Decide who buys the parts, and write the risk with them

Choose turnkey, consigned, or the standard hybrid: critical and allocated parts consigned, the commodity tail turnkey, and put the component-market risks on paper in the same clause: channel policy with franchised distribution first and brokers only under a written inspection practice, excess and end-of-life liability, attrition allowances, and who authorizes a lifetime buy. The parts market has cycles; the contract should already know that.

05

Buy test as engineering, not inspection

Specify the test strategy with the build: optical inspection as table stakes, X-ray wherever packages hide their joints, the flying-probe-versus-fixtured-test decision made on volume arithmetic you have seen, and functional test against limits you define. Ask what coverage the strategy reaches, in writing. Untested capability ships as field returns, and a supplier's answer to the coverage question previews everything else.

06

Gate the introduction, own the data, keep it portable

Run NPI as a gated path: DFM review before boards are ordered, first articles against drawing and class tied to acceptance and payment, and process documentation that survives handoff. Record ownership of stencils, fixtures, and test programs with their data, because a program whose data lives only at one supplier isn't portable when portability matters. This platform's tooled sectors all run this discipline; here the tooling is smaller, and the data matters more.

Glossary

Electronics Manufacturing Glossary: Key Terms Explained

The terms you will meet on a quote, a BOM scrub, or a first-article report, in plain English.

30 terms

Allocation

The component market's recurring weather: demand outrunning supply until manufacturers ration deliveries, lead times stretch from weeks to months, and buyers meet the gray market for the first time. Allocation cycles are why alternates are approved in advance, why lifetime-buy authority is assigned before scarcity, and why a supplier's channel discipline is a specification item rather than their private business.

Automated optical inspectionAOI

Camera-based inspection of assembled boards against the design data, catching missing, shifted, and misoriented parts and most solder defects at line speed. AOI is the workhorse verification behind the acceptability standards, and asking where it sits in a supplier's line, after paste, after placement, after reflow, is a fair and revealing process question.

Ball grid arrayBGA

The package family whose connections are solder balls underneath the part, invisible after soldering, which is why BGA work is judged by X-ray rather than eyesight. BGAs raise the technology floor of a job: fine ball pitches, voiding limits, and rework skill all become supplier-selection questions the moment one lands on the bill of materials.

Bill of materialsBOM

The parts list that is functionally the product's specification: every line is a manufacturer part number with its approved manufacturers, reference designators, and quantities, plus the do-not-place notes. Quotes are only comparable when the BOM is complete and current, and most quoting delays trace to lines that are ambiguous, obsolete, or missing their approved alternates.

Bottom-terminated components

The leadless package families, QFN and DFN chief among them, whose connections are pads under the body, as common as BGAs on industrial boards and raising the same questions: joints judged by X-ray rather than eyesight, voiding watched, rework a skill rather than a touch-up. Their presence on a BOM belongs in the technology-floor conversation, and their thermal pads are a classic DFM topic the review should reach before the stencil does.

Box build

Assembly beyond the board: enclosures, wiring, displays, sub-assemblies, loaded software, and packaging, up to a finished, tested product shipped under your label. Box build moves the supplier relationship from board vendor toward manufacturing partner, and it pulls in the adjacent purchases, enclosures from the sheet metal world, harnesses from theirs, under one roof or one coordinator.

Component lifecycle

Where each part stands in its maker's catalog: active, not recommended for new designs (NRND), end of life (EOL), or discontinued. Lifecycle is screened at the BOM line level before quoting, because a single dying part can force a redesign, a lifetime buy, or a broker hunt, and the screen is cheap while the surprise is not.

Conformal coating

The thin protective film applied over an assembled board against moisture, condensation, and contamination, specified by material family, coverage areas, and keep-out zones. Coating is a process with its own acceptance criteria, and a drawing that marks what must be coated and what must stay bare has prevented the classic masking dispute.

Consigned and turnkey

The sector's two commercial models: consigned, where you buy the components and the assembler provides labor and process, and turnkey, where the assembler buys everything against your approved list. Hybrids are common: consigning critical or allocated parts while the assembler buys commodity lines, and the choice shifts procurement risk more than it changes the board.

Counterfeit components

Parts that are not what their markings claim: remarked date codes, refurbished pulls, or outright fakes that enter through unauthorized channels and fail later. The defense is channel discipline: franchised distribution first, independent sources only under a stated inspection and traceability policy, because a counterfeit is a field failure with a purchase order behind it.

Design data package

The files that define the board and the build: fabrication data in Gerber or ODB++ formats, drill files, the BOM, assembly drawings, and pick-and-place centroids. It is the specification the quote is priced from and the asset your portability depends on, so completeness is checked at RFQ time and ownership is written down.

Design for manufacturabilityDFM

The review that reconciles a design with the process that must build it: footprints, spacings, panel layout, testability, and solderability, fed back before boards are ordered. A supplier's DFM comments are free engineering and a preview of their seriousness, and the cheapest changes in this sector are the ones made before the first article exists.

First article inspectionFAI

Full verification of initial assemblies against the drawing and acceptance class; the qualification gate before quantity production, with the aerospace world formalizing it as the AS9102 report. It is where new product introduction hands off to production, and tying it to acceptance and payment is standard discipline rather than distrust.

Flying probe test

Electrical test by moving probes rather than a fixed fixture: slower per board, but with no fixture to build, which is why it owns prototypes and low volumes. The crossover to fixtured in-circuit test is an arithmetic of volume against fixture cost, and a supplier should be able to show that arithmetic on request.

Functional test

Testing the assembly as the product: powered, exercised through its real behavior, against pass and fail limits you define. Functional test finds what structural tests cannot, and its fixtures and programs are engineered items, owned, documented, and portable by the same rules as any other tooling.

High-density interconnectHDI

Board construction using microvias, very fine traces, and thin dielectrics to route fine-pitch parts, built by a narrower set of fabricators with laser drilling and sequential lamination. HDI on a design is a supplier-sorting fact on the bare-board side and a cost driver worth confirming early, because not every board shop lives there.

In-circuit testICT

Electrical test through a bed-of-nails fixture pressing on designed-in test points, verifying components and connections quickly at volume. The fixture is a per-design engineering charge, which is why ICT belongs to production quantities, why test points belong in the layout from the start, and why the fixture's ownership belongs in the order.

IPC classes

The three-level language of how good the work must be: Class 1 for general electronics, Class 2 for dedicated-service products that must be reliable, Class 3 for high-reliability work where failure is not acceptable. The class drives cost, inspection, and process control; it is specified in writing with the standard and revision named, and exceptions can be drawn per reference designator when only part of a board is critical.

Laminate and glass transition

The board's base material and the temperature behavior that selects it: the glass-epoxy family at the center, graded by glass transition temperature, the point where the resin softens and expansion accelerates, with higher-performance resins beyond for thermal, frequency, and reliability demands. Laminate is chosen based on assembly temperatures and service life; it is a real cost driver and a fabricator-sorting fact, and it is named on the fabrication drawing, not inherited.

Moisture sensitivity levelMSL

The rating on moisture-sensitive packages states how long they may sit in factory air before soldering: level 1 is unlimited, the middle levels count down, level 3 allows one week, and level 6 requires baking before use. Absorbed moisture flashing to steam in reflow cracks packages from within, so dry storage, cumulative floor-life clocks, and baking discipline are things a serious assembler can show you.

New product introductionNPI

The structured path from design files to repeatable production: DFM review, prototype builds, test development, first articles, and the process documentation that survives the handoff. NPI is a service worth buying deliberately, and the classic mistake is treating a prototype vendor's heroics as evidence of production readiness, in either direction.

Panelization

Building boards in multi-up panels joined by breakaway tabs or scored routes, the format assembly lines actually run. Panel layout is decided with the assembler during DFM; it affects price through utilization and handling, and the depaneling method is specified because tab remnants and stresses land at board edges where connectors like to live.

Reflow soldering

The core surface-mount process: printed solder paste, placed parts, and a tuned journey through a reflow oven whose profile melts and forms every joint at once, with lead-free alloys peaking around 250 degrees Celsius. The profile is engineering, not a setting, which is why moisture-sensitive parts, laminate choices, and large thermal masses all come up in process conversations.

Restriction of Hazardous SubstancesRoHS

The regulatory regime restricts lead and other substances in electronics sold in many markets; this is why lead-free soldering is the default and exemptions are declared rather than assumed. Compliance travels with declarations and material data through the supply chain, and an RFQ states the target markets so the build is compliant where the product will actually go.

Selective soldering and through-hole (THT)

The processes for leaded parts on otherwise surface-mount boards: wave soldering for through-hole-heavy designs, selective soldering machines for the few connectors and headers surface-mount designs still carry, and hand soldering, governed by the same process standard, at the small end. Mixed-technology boards are normal; the mix belongs in the quote because it drives routing and labor.

Solder paste and stencil

The paste of powdered alloy and flux printed onto pads through a laser-cut stencil, the step where most soldering quality is actually decided. The stencil is a per-design tool with an owner; printing is monitored by inspection, and paste discipline, storage, life, and handling, is one of the quiet markers of a well-run line.

Stackup

The board's construction recipe: layer count, copper weights, dielectric materials, and thicknesses, agreed between designer and fabricator. Stackup determines cost and which fabricators can quote, and it specifies controlled impedance rather than hoping for it: signals that need defined impedance get called out, the fabricator tunes geometry to hit them, and test coupons on the panel prove it. Confirming stackup with the board shop before release is the bare-board version of the strip-layout review, cheap early and expensive late.

Surface finishes

The coating on the bare board's copper that keeps it solderable: hot air solder leveling (HASL), the economical legacy finish, and electroless nickel immersion gold (ENIG), which flat-finish fine-pitch work prefers, among others. The finish is chosen based on the component mix and shelf-life needs, as noted on the fabrication drawing, and confirmed rather than left to a default.

Surface-mount technologySMT

The dominant assembly technology: components placed onto printed solder paste and reflowed, at machine speeds, with passive parts down to the 01005 size, smaller than a grain of sand. SMT capability defines an assembler's technology floor, so the smallest package and finest pitch on your BOM are supplier-selection facts, not trivia.

X-ray inspection

Inspection that sees through packages to the joints beneath them, the only way to judge BGA and bottom-terminated solder connections, voiding above all. If the design carries hidden-joint packages, X-ray belongs in the process and in the quote, and asking to see a sample image is a fair capability check.

Standards

Electronics Manufacturing Standards: IPC-A-610, J-STD-001, and the Class System

What each standard governs and why a buyer should care. Which ones apply depends on the scope of the work, the markets the product serves, and how much a failure would cost.

Assembly acceptance and process standards

IPC-A-610 acceptability of electronic assemblies

Published by IPC, the electronics industry association: the acceptance standard for assembled boards, the visual and written criteria for solder joints, placement, and artistry that define what a finished assembly may look like, graded by the three classes. It applies to essentially every assembly purchase, cited or assumed. Its buyer leverage is the citation itself: name the standard, the revision, and the class in writing on the drawing or purchase order, because the class changes cost and inspection honestly, and an assembly judged without a named class is judged by whoever inspects last.

J-STD-001 soldered assembly requirements

Published by IPC: the process standard for soldered electrical and electronic assemblies, the how-it-is-built companion to the acceptance standard's what-may-ship, covering materials, methods, and process control, in the same three classes. The pair travel together: a Class 3 program means Class 3 process control and Class 3 acceptance, not one without the other. For a buyer, its presence signals capability; operator certification is checkable, and naming both standards in the order is how artistry stops being a conversation.

IPC/WHMA-A-620 cable and harness assemblies

Published jointly by IPC and WHMA: the acceptance standard for cable, wire, and harness assemblies, the same class logic applied to the wired world. It appears here as a boundary marker: when the work is harnesses rather than boards, the standard changes, the supplier base changes, and this platform's wire, cable, and harness page carries that sector from its own side. On mixed products, box builds with internal wiring, both standards can apply, each to its own scope, and stating that split keeps two inspectors from arguing over one cable.

Board, design, and component-handling standards

IPC-A-600 and IPC-6012 for bare boards

Published by IPC: the acceptability standard for printed boards, what a bare board may look like, and the qualification and performance specification for rigid boards, what it must be, plating, hole quality, and construction, with market-specific sheets extending it for automotive, medical, and space work. They apply to every bare-board purchase, and they complete the class formula: a genuinely Class 3 product is board, process, and acceptance together, and the string a serious specification writes out is exactly this: IPC-6012 Class 3, J-STD-001 Class 3, IPC-A-610 Class 3, written in full because the classes do not flow automatically from one document to the next.

IPC-2221 design standards family

Published by IPC: the generic design standard for printed boards, conductor spacing, current capacity, and the physical rules a manufacturable layout obeys, with its family of sectional standards beneath it. Buyers rarely open it; designers live in it; and its buyer relevance is the handshake it enables: a design done to the standard family arrives at fabrication and assembly speaking the same dimensional language the DFM review will use, which is why sophisticated RFQs mention the design basis alongside the data package.

J-STD-020 and J-STD-033 moisture sensitivity

Published jointly by IPC and JEDEC: the classification standard that rates moisture-sensitive packages, levels 1 through 6, and the handling standard that governs their dry storage, floor-life clocks, and baking. Absorbed moisture flashing to steam in the reflow oven cracks packages invisibly, so the rules are unforgiving: level 1 has unlimited floor life, level 3 gets a week of cumulative exposure (168 hours by the book), and level 6 is baked before use. For a buyer, this pair is an audit shortcut: ask how floor life is tracked and when parts are baked, and the answer tells you how the whole stockroom is run.

Quality systems, market gates, and the institutional anchor

ISO 9001

Published by the International Organization for Standardization: the general quality management system standard, the baseline registration most contract manufacturers hold, covering document control, traceability, corrective action, and calibration a buyer leans on without naming them. It is the floor of qualification, not the ceiling: registration says the system exists, and says nothing about fine-pitch capability, test depth, or class discipline, which is why the certificate check begins the conversation that the line tour, sample boards, and references finish.

Sector gates: AS9100, ISO 13485, IATF 16949

Published by their industry bodies as the quality systems layered onto the general standard for aerospace, medical devices, and automotive, respectively. They arrive as flowdowns: if your product feeds those chains, the requirement comes from your customer, and the supplier search filters to manufacturers holding the registration before any board is discussed. For medical work, the gate leads next door; this platform's medical device contract manufacturing page covers that regime's world, and for buyers outside these chains, the registrations remain useful signals with overhead priced in.

ITAR and export control

Administered separately: ITAR by the U.S. State Department, and the export administration regulations beside it by the Commerce Department, the export-control regimes governing defense articles and controlled technical data, under which defense electronics work requires registered manufacturers, controlled data handling, and attention to who may touch the files at all. It applies the moment a design is defense-controlled, and it applies to the RFQ itself, since sending controlled data to an unregistered or offshore supplier violates the rules before any part is built. Buyer discipline is to confirm the design's control status first and filter the supplier list by registration, stated plainly and early.

AS5553 and AS6081 counterfeit avoidance

Published by SAE International: the counterfeit-parts avoidance standards, one for organizations that buy and build, one for the distributors they buy through, defining the risk assessment, sourcing hierarchy, inspection, and traceability that keep fraudulent parts out of assemblies. Born in aerospace and defense, their logic travels everywhere allocation pushes buyers toward independent channels. The buyer content is the policy question: ask any turnkey supplier what their counterfeit-avoidance practice is, through what channels they buy, and what happens when only a broker has the part, and expect a written answer.

IPC, the industry's standards body and anchor

IPC, the electronics manufacturing industry association, publishes the core standards on this page, several jointly with WHMA and JEDEC, and runs the certification programs behind them, the certified specialist and trainer credentials an assembler's inspectors and operators hold and renew. It convenes the industry rather than regulating it, and nothing it publishes is mandatory until a contract makes it so, which is precisely the buyer's move: the standards become binding because your purchase order names them. A supplier's IPC engagement, memberships, and certifications on the floor is one honest signal of seriousness in a sector where process discipline is the product.

Frequently Asked Questions

Electronics Manufacturing FAQs

Direct answers to the questions buyers ask most often when sourcing in this sector.

Match the door to the scope. Bare-board fabricators build the unpopulated board from your fabrication data; a photochemical and drilling business with its own quick-turn and volume tiers. Assembly houses and EMS providers populate boards, and at scale they procure the components, build the box, load the software, test the product, and ship it under your label. The practical sort: board files alone go to a fabricator; boards plus a BOM go to an assembler, most of whom will arrange the bare boards; a product goes to an EMS partner scoped for box build and test. Two more filters decide who can actually bid: the technology floor, the finest pitch, smallest passives, and any HDI construction on your design, and the volume-and-mix band, since prototype shops, high-mix mid-volume houses, and high-volume lines are different businesses wearing one industry's name.

They are the industry's three-step answer to how good the work must be. Class 1 is general electronics, where cost rules and a cosmetic defect is tolerable. Class 2 is dedicated-service equipment, products that must work reliably for years, and it is the sensible default for most industrial hardware, which is also what you get when nobody asks. Class 3 is high-reliability work, medical, aerospace, defense, anything where failure injures someone or ends a mission, and it prices accordingly through tighter criteria, slower lines, and more inspection. Specify by writing it down: the standard, the revision, and the class on the drawing or order, remembering that the full Class 3 string is written out in full, IPC-6012 Class 3, J-STD-001 Class 3, IPC-A-610 Class 3, because the classes do not flow automatically from one document to the others, and that exceptions can run per reference designator when one circuit is critical and the rest of the board is not.

A complete package, because the quote is priced from files, not descriptions. The BOM with manufacturer part numbers, approved manufacturers and alternates, reference designators, and do-not-place notes. The design data: fabrication files in Gerber or ODB++, drill data, assembly drawings, and pick-and-place centroids. The acceptance class in writing, with any per-designator exceptions. Quantities and the release pattern: prototypes, pilot, production bands, since price breaks and process choices hang on them. The test expectation, even roughly stated. And the commercial stance: turnkey or consigned, target markets for regulatory compliance, and whether bare boards are in the assembler's scope. Incomplete packages do get quoted, slowly, with assumptions attached, and every assumption is a change order in the making.

Turnkey, where the assembler buys everything against your approved list, buys you their purchasing leverage, their incoming inspection, and one throat to choke, at a material markup that is usually cheaper than running board-level procurement yourself. Consignment keeps component sourcing, cost, and risk in your hands, and makes sense when you already buy the parts at scale, hold allocation relationships, or face controlled-sourcing rules. The working answer for most programs is the hybrid: consign the critical, allocated, or customer-directed parts, and let the assembler buy the commodity tail. Whatever the split, write down the risk terms that travel with it: who owns excess and end-of-life buys, what attrition allowance applies, and whose problem a lot failure is, because those questions only feel theoretical until the first constrained part.

Because assembly is fast and parts are not: the line turns boards in days, while a single constrained or dying component sets the calendar for everything. The protections are unglamorous and early. Screen the BOM for lifecycle before quoting; end-of-life and not-recommended parts are redesigns waiting politely. Approve alternates line by line in advance, so a substitution is a lookup instead of an engineering hold. State the channel policy: franchised distribution first, independent sources only under a written inspection and traceability practice, because the gray market is where counterfeits live, and allocation is when buyers visit it. And decide the risk-buy questions: who authorizes lifetime buys, who owns the excess, before scarcity decides them for you. Allocation cycles recur in this industry; programs that survive them are planned for them at RFQ time.

Buy it as a strategy, not a checkbox. In-process verification comes with a serious line: automated optical inspection against the design data, and X-ray wherever hidden-joint packages put solder where eyes cannot go. Electrical test is an economic choice you should see the arithmetic for: flying probe needs no fixture and owns prototypes and low volumes, while in-circuit test through a bed-of-nails fixture is fast per board and pays for its fixture at production quantities, provided test points were designed in. Functional test, the product exercised as a product against limits you define, catches what structure cannot. State the expectation in the RFQ, ask what coverage the proposed strategy actually reaches, and treat fixtures and test programs as owned, documented tooling, because that is what they are.

New product introduction is the engineered path from files to repeatable manufacturing: the DFM review that reconciles design with process, prototype builds, test development, first articles against the drawing and class, and the documentation that makes build ten identical to build two. What changes at production is the center of gravity: from engineering attention and fast turns to process stability, yield, and cost, sometimes at the same supplier, sometimes not, since prototype heroics and production discipline are different talents. The buyer's discipline is the gate: first-article approval, tied to acceptance and payment, marks the handoff, and the honest conversation about whether your NPI partner is your production partner happens before you commit volumes, not after the first late delivery.

Whoever the paper says, which is why the paper should say. Stencils, in-circuit fixtures, functional test rigs, and test programs are per-design engineering, usually billed as one-time charges. Under this platform's standing rule, the buyer who pays for tooling owns them, with their location and data recorded. Ownership without the data is decorative: the design package, test programs, and process documentation are what make a program portable to a second source or a successor supplier, so data rights travel in the same clause. None of this signals distrust; it is the same discipline every tooled sector on this platform runs, and suppliers who work at any scale expect the conversation and respect the buyer who has it.

Split the question the way the industry does. Assembly itself is quick: quick-turn prototypes run in days, production assembly in days to a few weeks once parts are staged. Bare boards run from days on domestic quick-turn to several weeks for complex or offshore fabrication. Components are the honest answer's center: stocked parts arrive this week, and constrained parts are quoted in months, which is why the parts strategy in the questions above is really the schedule strategy. Fixtures and NPI add their own first-build weeks. A supplier's quote should show these clocks separately: staged material, board fabrication, assembly, test, and a quote that shows one blended number has answered a simpler question than the one you asked.

Buyer's Guides

Guides for Sourcing Electronics Manufacturing

In-depth guides covering the decisions above.

Buyer's Guide

Choosing an Electronics Contract Manufacturer: IPC Classes and Capabilities

What the IPC class decision actually changes, the standards that govern each stage, capability, component sourcing, test strategy, and how to read a quote.

Read the guide

More coming

This sector is growing.

Additional guides are added when there is something genuinely worth saying, not on a schedule. IWS is committed to providing educational content to help you find the right suppliers!

Downloadable Resources

Electronics Manufacturing Downloads: Checklists and Reference Tools

Practical tools you can take into a supplier conversation.

Find a verified electronics manufacturing supplier

Search the network for verified manufacturers, distributors, and service providers in this sector.

Every supplier verified · No pay-to-rank

Can't find it? We'll find it for you, free.

Tell us exactly what you require. Our team has spent 30+ years in industrial supply chains, and we'll track down qualified suppliers within one business day. No cost, no obligation.

Request Free Sourcing Help
